DISTRIBUTOR-FIRST SUPPLY PARTNER · SINCE 1999 Live · Pneumatic Automation System
SPC Company
Pneumatic Automation / Control & Valving / Directional Control Valves / ATEX Solenoid Valve
Layer 03 · Control & Valving Value · AIGNEP
What it is

ATEX Solenoid Valve

Compare tiers ↓

An ATEX solenoid valve is a directional control valve certified as a complete unit, valve body and coil together, for use in classified hazardous (explosive-atmosphere) areas. ATEX (Atmosphères Explosibles, the EU directive governing equipment in explosive atmospheres) is the European framework; Class/Division/Group is the equivalent North American framework. The valve carries a permanent marking that names the exact zone or class it is approved for, and it installs in the classified area as a single drop-in component. It is the right product on every cylinder in oil and gas, chemical, petrochemical, refining, grain handling, paint booths, pharma solvent suites, and underground mining.
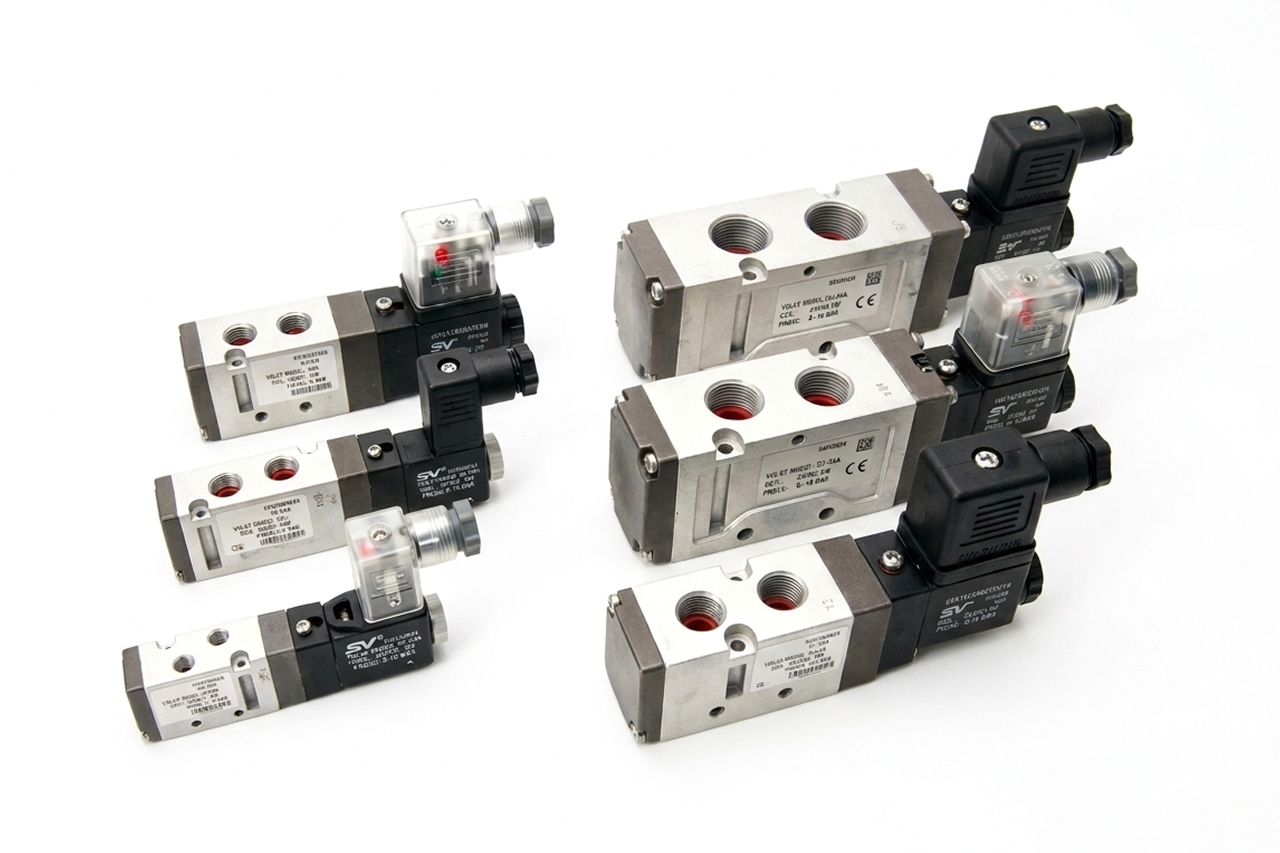
Pictorial Representative atex solenoid valve
ATEX Solenoid Valve — representative illustration
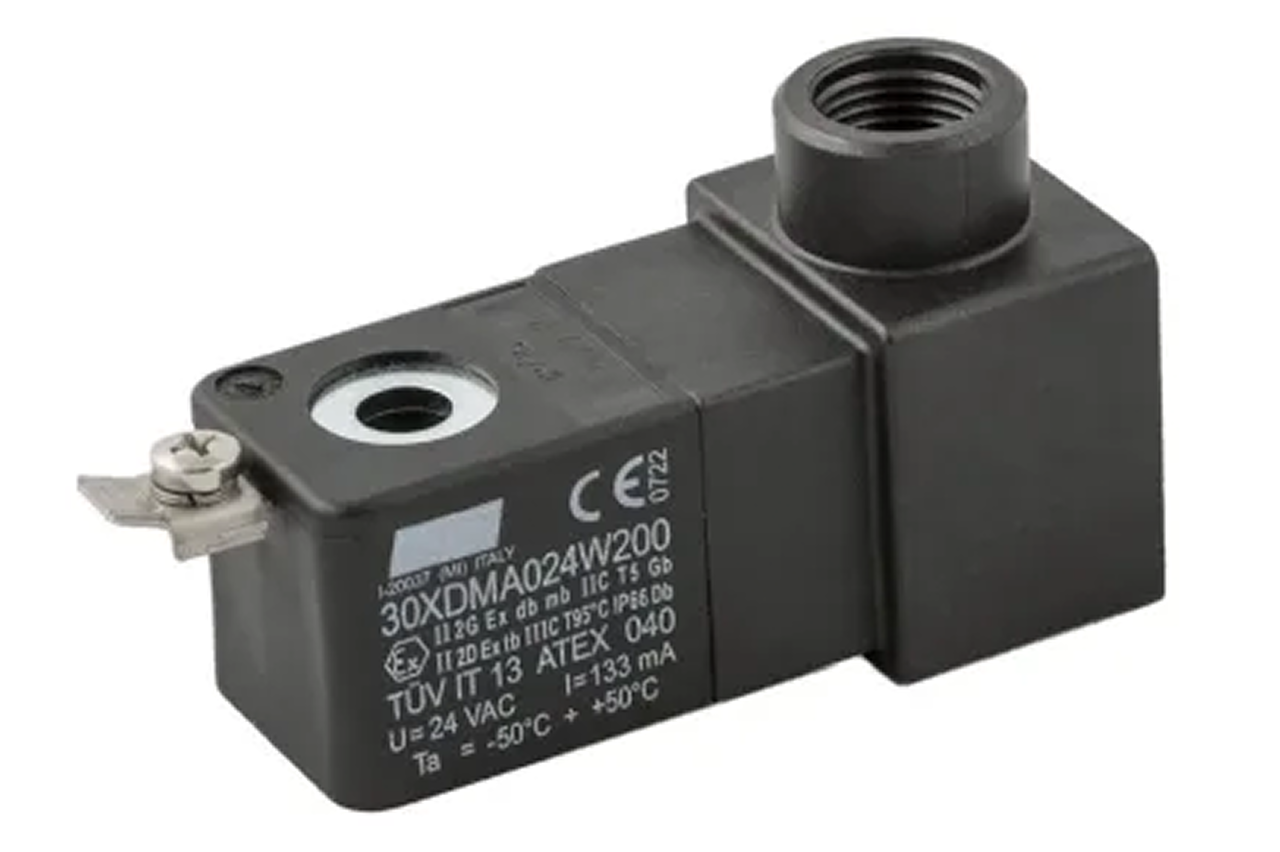
Real-world reference Representative atex solenoid valve
ATEX Solenoid Valve — representative product photo
Why it's needed

Why this matters.

When the ATEX-certified valve is the right call, and when to spec something else. Review the points below.

01 · Key point
Valve and coil certified together.

One marked unit covers valve body and coil, spark-suppressed winding, surface-temperature limit below the gas autoignition temp, enclosure that contains internal ignition. Drops in like a standard valve; one certificate of conformity per install.

02 · Key point
The marking is the legal spec.

Permanent body marking lists the exact Class/Division/Group (North America) or ATEX zone, gas group, T-class (Europe). Audit reads the marking, not the catalog. Illegible = unverifiable = non-compliant under most inspection protocols.

03 · Key point
The certified brand ships the documentation.

A leading-tier ATEX brand supplies unit-certified valves with documented zone coverage, EU certificate of conformity, and the marking sheet. Ship the digital cert packet at sale: customers lose paper certs and the next OSHA audit asks for them.

04 · Pro tip
Consider the air-piloted alternative.

Where the zone permits, place a standard solenoid in a safe area and run a pilot line to a non-electrical pilot-operated DCV at the cylinder. Functionally equivalent, often cheaper than a single unit-certified valve, faster supply chain. Customer-confirm against the area drawing.

05 · Where not to use
Mismatched certification scope.

Zone 1 IIB T4 is not interchangeable with Zone 2 IIA T3. A near-match voids compliance and the auditor will find it. → Verify body marking character-for-character against the area-classification drawing before quoting.

06 · Where not to use
Partial-certified pneumatic trains.

A certified valve discharging into a non-certified FRL or cylinder defeats the safety design and fails audit. → Either the whole train inside the zone is certified, or downstream components live outside the zone with sealed boundary fittings.

07 · Where not to use
Outside the hazardous area.

No certification means no install penalty, no documentation overhead, faster lead time. → Re-spec to standard solenoid for safe-area applications. Confirm the install location against the area drawing before defaulting to ATEX cost.

Key selection criteria

What we need to spec it right.

From the machine spec sheet to the part number. Answer what you know, leave the rest blank, and send.

04Choose your priority  ·  core differentiator

Whatever your lever — performance, value, or price — SPC has the right brand.

Pick the priority; the quote desk handles the cross-reference.

02 Value 1 brand
Install · 6 critical steps

The things that matter on the first install.

Step 01
Verify the certification marking matches the area classification before mounting
The marking on the valve body lists the exact zone/gas group/temperature class (ATEX) or class/division/group (North American). Compare character-for-character to the area-classification drawing for the install location. A near-match is not a match: Zone 1 IIB T4 is not interchangeable with Zone 2 IIA T3. If the marking and the area do not align exactly, stop and reconcile before installing.
Step 02
Match coil voltage and respect the certified-pigtail-only wiring requirement
ATEX coils typically ship with a manufacturer-certified cable pigtail and prohibit field-cutting that cable, cutting voids the certification. Read the install manual for cable-length and termination requirements before pulling the install. Coil voltage match (24 VDC, 110 VAC, 220 VAC) is verified exactly as for standard solenoids; wrong voltage burns the coil and breaches the certification.
Step 03
Plumb to ATEX-rated downstream components, not standard ones
A certified valve discharging into a standard non-rated cylinder, FRL, or piping defeats the safety design. If only the valve is certified, the cylinder and piping must live outside the zone with hose passing through a sealed wall fitting into the hazardous area.
Step 04
Retain the certificate of conformity in the plant maintenance file
The certificate (EU Declaration of Conformity for ATEX; the manufacturer's certification letter for North American CSA/UL/FM) is part of the plant's permit-to-operate documentation. Provide a digital copy with the shipment and document the file location.
Step 05
Add the valve to the plant's hazardous-area inventory
Most plants maintain a running inventory of certified components by location, scope, install date, and inspection schedule. The valve install is the moment to add the entry, retroactive entries rarely happen.
Step 06
Schedule the recertification or inspection interval per local code
ATEX and Class/Division certifications typically require periodic inspection (annual to triennial depending on zone severity) to confirm the marking is legible, the coil pigtail is intact, and no contamination or damage has voided the certified state.
Troubleshoot · top failures

Most returns trace to one of these causes.

Symptom
Most likely cause
Fix
Valve operates correctly but a plant audit flags the install as non-compliant
Certification marking does not match the area-classification drawing for the install location, or the certificate of conformity is missing from the plant maintenance file, or the certified pigtail has been field-cut.
Document the actual marking and compare to the area class. If mismatched, replace with a valve whose scope covers the area. If the certificate is missing, request a re-issued document from the manufacturer. If the pigtail has been cut, the certification is voided, replace, or have the manufacturer re-certify per their documented procedure.
Continuous air leak from valve body in a hazardous area
Same root causes as a standard solenoid (seal damage, body crack), but in a hazardous area the leak itself can be a hazardous-area event, escaping air may contain process gases or vent into the classified atmosphere.
Immediate isolation and replacement. Do not field-disassemble a certified valve in a hazardous area without manufacturer service authorization, field repair voids the certification. Replace with a new certified unit; ship the failed unit for failure analysis if there is a contamination or service-life concern.
Coil heats excessively in normal operation
Duty rating exceeded, ambient outside coil rating (hazardous-area enclosures run hotter than open-air), or sustained over-voltage condition.
Check coil rating against actual ambient and duty cycle. If within rating, measure supply voltage at the coil under load, sustained over-voltage burns coils and elevates surface temperature, both of which compromise the temperature-class certification. Correct the source or specify a higher-rated coil.
Audit flags certified valve downstream of a non-certified FRL or cylinder
Partial certification, only the valve is rated; the rest of the pneumatic train is standard. System-design issue, not a valve issue, but it surfaces at audit and the valve quote often gets blamed.
The entire pneumatic train inside the zone must be either certified or relocated outside the zone with appropriate boundary fittings. Recheck the original design; upgrade downstream components or relocate them.
Valve has been in service ~5 years and the body marking is no longer fully legible
Marking degradation from solvent exposure, abrasion, or sun (outdoor installs).
Replace the valve. The marking is the legal evidence of certification; an illegible marking means an unverifiable scope. Re-issuance of the marking is generally not a field service. Even when the valve still functions correctly, illegibility is a non-compliant condition under most inspection protocols.

Get the right atex solenoid valve on quote in 24 hours.

Send us the application — a specialist routes you to the correct tier with a configured part. Lead-times and pricing returned within one business day.

Open quote engine ↑