DISTRIBUTOR-FIRST SUPPLY PARTNER · SINCE 1999 Live · Compressed Air System
SPC Company
Compressed Air / Generation / Air Compressors / Rotary Screw Compressor — Fixed-Speed
Layer 01 · Generation Performance · Chicago Pneumatic Value · CASTAIR Price · ABAC
What it is

Rotary Screw Compressor — Fixed-Speed

Compare tiers ↓

A rotary screw compressor, fixed-speed is a continuous-duty industrial compressor whose motor runs at one constant speed and whose airend (the compression element, two intermeshing helical rotors in a close-fitting housing) feeds a single shared receiver tank. It is the default compressor for any operation that runs air all day, sized from 5 HP up past 500 HP and rated for 100% duty cycle. It sits in the generation layer at the head of the compressed air system, ahead of the receiver, dryer, filtration, and distribution piping.
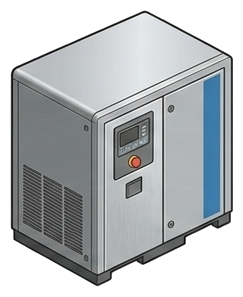
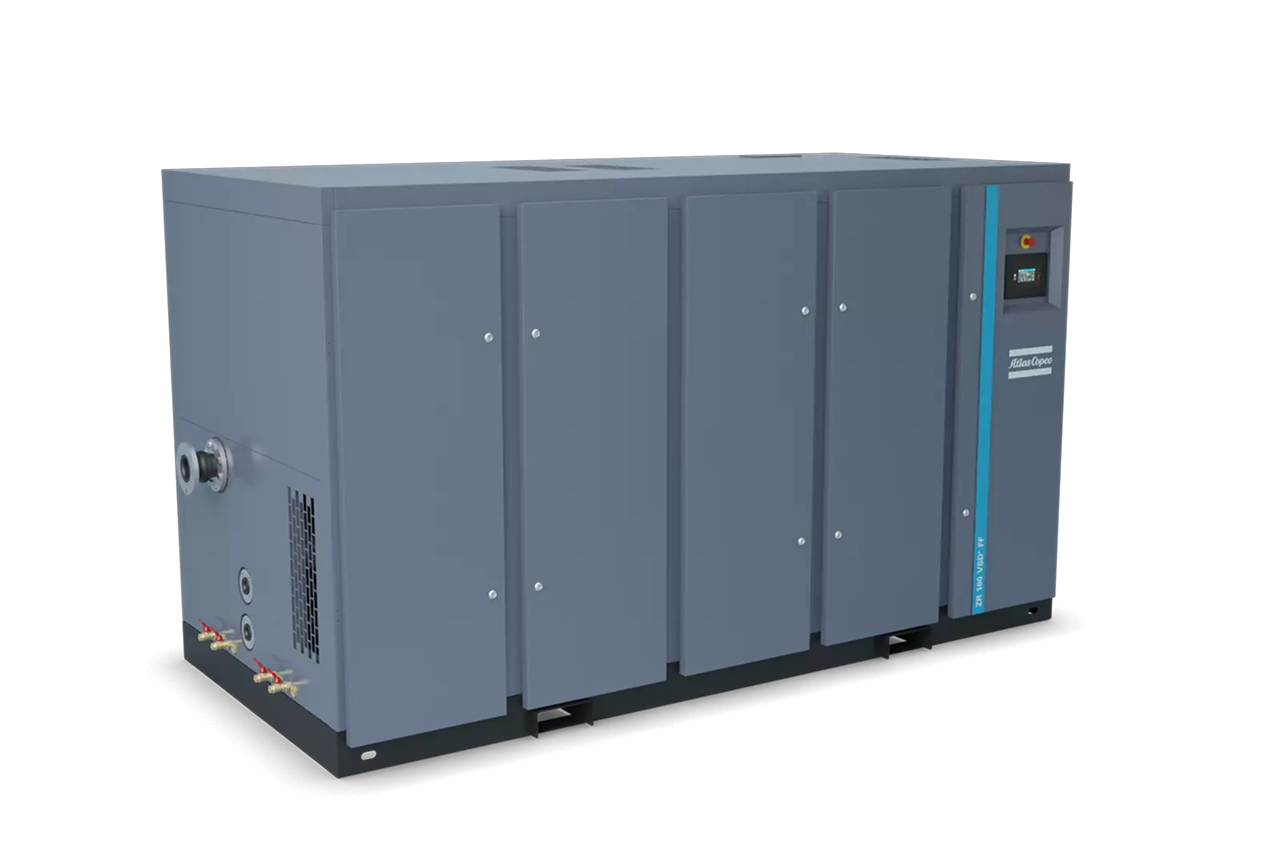
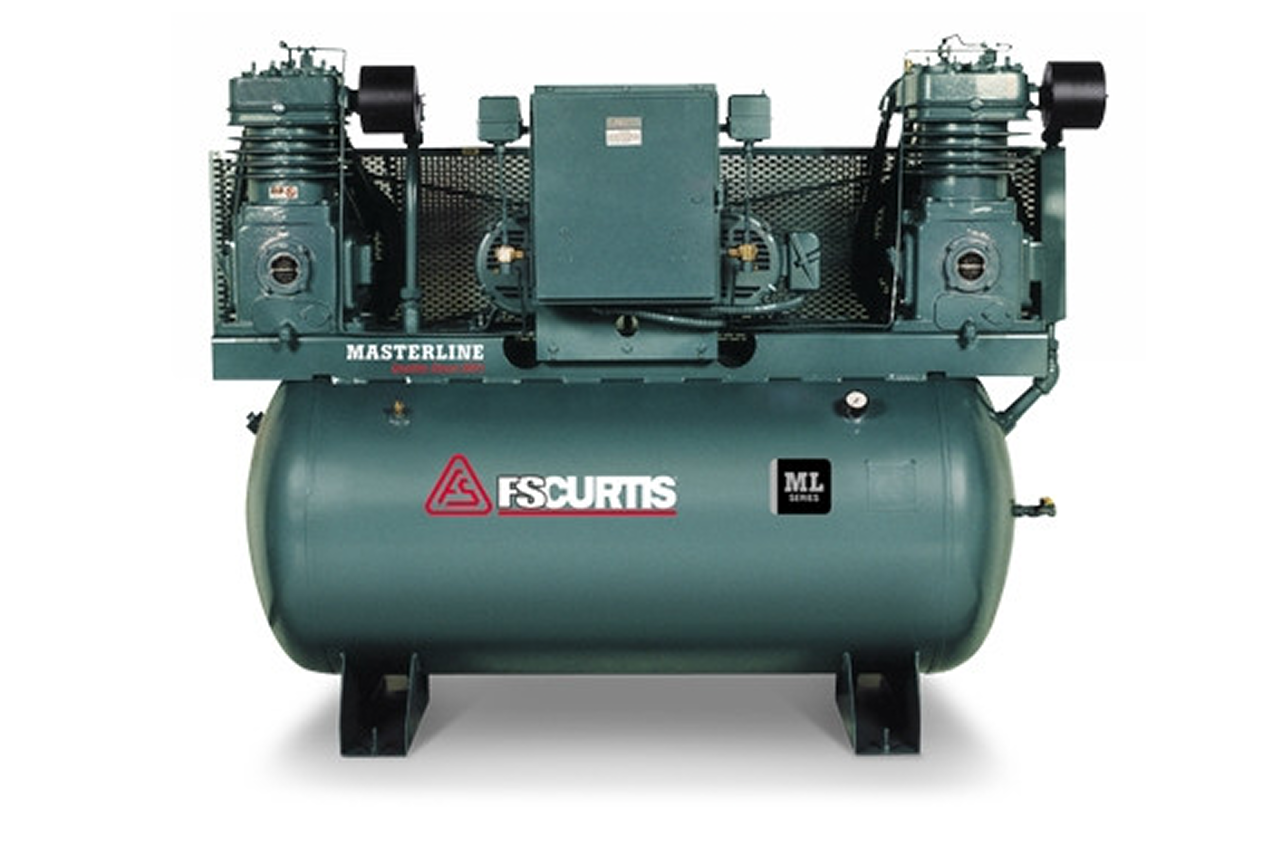
Pictorial Representative rotary screw compressor — fixed-speed
Rotary Screw Compressor — Fixed-Speed — representative illustration
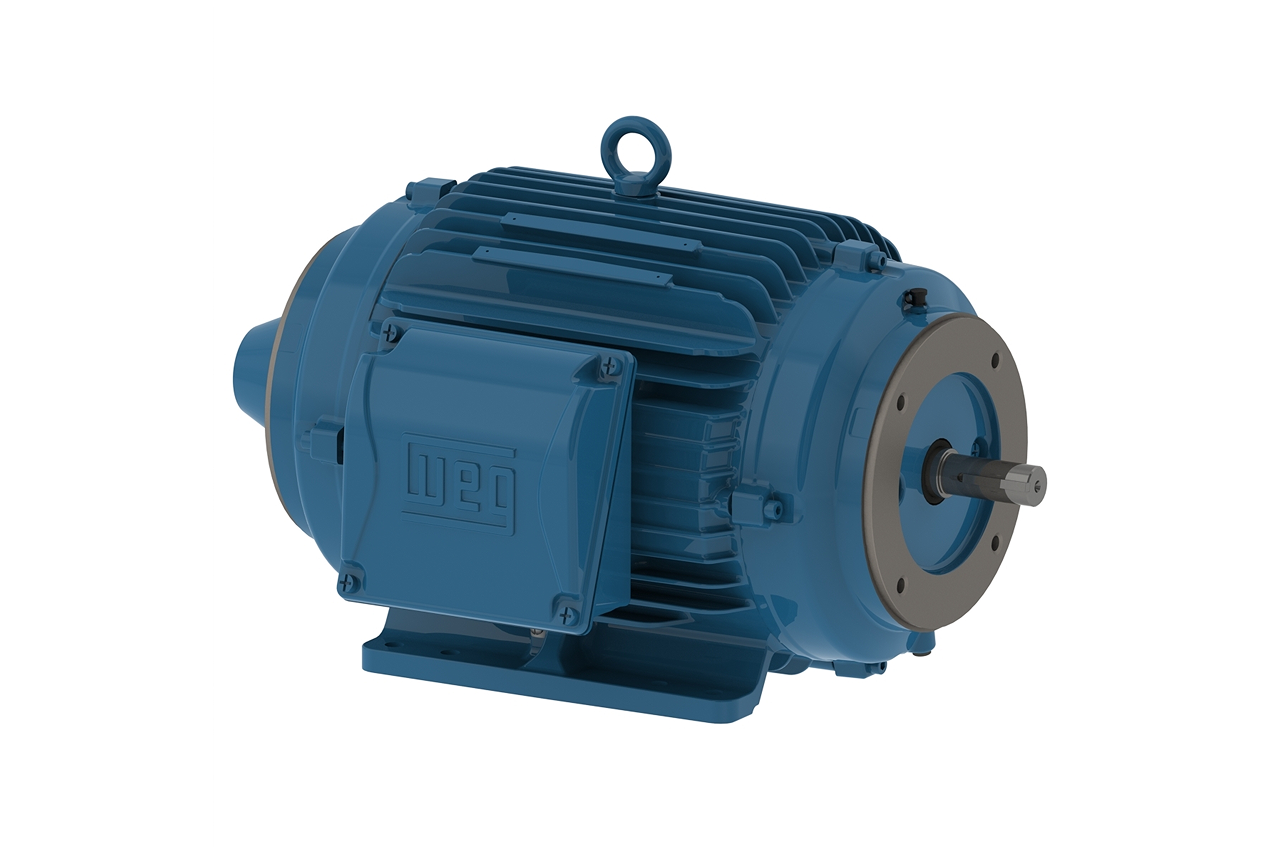
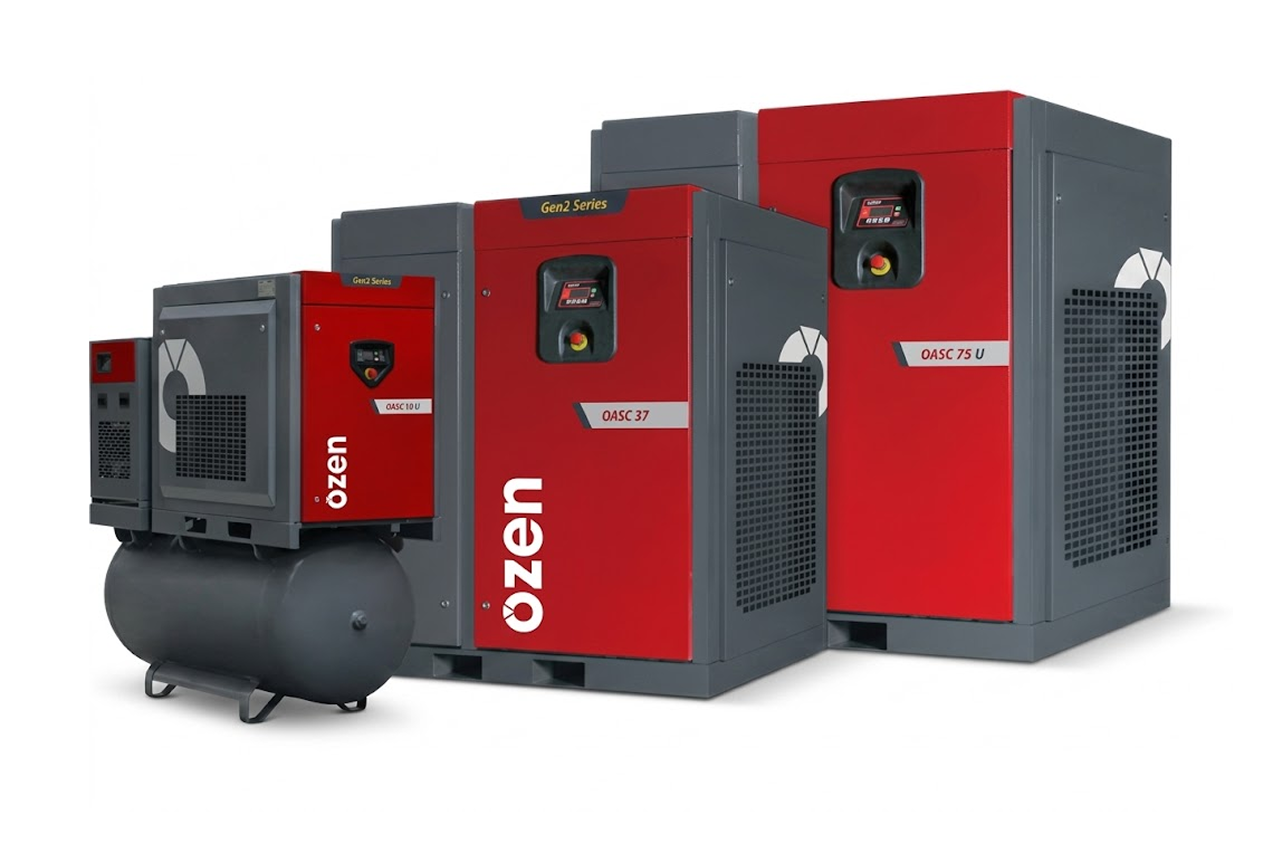
Real-world reference Representative rotary screw compressor — fixed-speed
Rotary Screw Compressor — Fixed-Speed — representative product photo
Why it's needed

Why this matters.

When fixed-speed rotary screw is the right call, and when a different compressor belongs on the quote. Review the points below.

01 · Key point
Continuous rotary, 100% duty.

Two intermeshing helical rotors compress air without stopping, no pistons reversing, no valves slapping. Rated for full-load operation around the clock; a production line at steady draw is the textbook fit.

02 · Key point
Quiet enough for in-plant.

60-75 dB versus 85+ dB on reciprocating. Installs inside the production envelope without a sound enclosure or a separate compressor room.

03 · Key point
Sized straight off the demand list.

Output runs ~4 CFM per HP at 100 PSI from 5 HP to 500+ HP. Pull peak demand, add 25% headroom, divide by four, the HP picks itself.

04 · Pro tip
Fixed-speed only when load is flat.

Load/unload control is efficient when demand sits near rated output. If air draw swings more than ~30% across a typical day, quote VFD instead: an unloaded motor still pulls 25-40% of full-load power for zero CFM.

05 · Where not to use
Intermittent shop duty.

A two-bay auto shop running an impact gun in bursts will spend most of the day unloaded and amortize a screw against a small revenue stream. → Re-spec to reciprocating when honest loaded time is under ~40 min/hr.

06 · Where not to use
Class 0 air-quality requirements.

Oil-injected feeds Class 1 with coalescing + carbon downstream, not Class 0. Food-direct-contact, pharma, electronics, fine finishing fail audit. → Switch to oil-free when an FDA / cGMP / ISO 8573-1 Class 0 spec is on the table.

07 · Where not to use
Hot rooms above 100°F at inlet.

Above 100°F ambient the compressor derates or trips on high-discharge-temp. → Fix the room first (ventilation, ducted intake) or spec a high-temp package, don't oversize the frame to mask a building problem.

RFQGuided system builder

Tell us about the shop. We size the system.

Answer a few plain questions and we build the full compressed air system for you: compressor, dryer, tank, filtration, and piping. No pricing here on purpose. SPC sizes, sources, and sends you an exact quote.

04Choose your priority  ·  core differentiator

Whatever your lever — performance, value, or price — SPC has the right brand.

Pick the priority; the quote desk handles the cross-reference.

01 Performance 2 brands
02 Value 2 brands
03 Price 1 brand
Install · 6 critical steps

The things that matter on the first install.

Step 01
Size both the receiver tank and the compressor
Rule: 3-5 gallons of receiver per CFM of output. A 50 HP unit at 200 CFM needs at least a 660-gallon receiver to buffer load/unload cycles. Undersized receiver = compressor cycling too frequently = airend wear + electric bill spike.
Step 02
Verify electrical capacity
Three-phase, voltage-matched to the panel. A 50 HP unit pulls ~140A at 480V; confirm breaker, conductors, and disconnect are sized correctly BEFORE delivery. Electricians prefer weeks ahead, not the day the compressor arrives.
Step 03
Cooling air or water management
Air-cooled needs ~250 CFM of cooling-air flow per 50 HP into the compressor room AND an equivalent path out. Without that, the compressor recirculates its own discharge heat and trips on high-temp fault within an hour. Water-cooled needs verified supply, drain, and freeze protection.
Step 04
Treatment downstream before commissioning
Refrigerated dryer plus particulate + coalescing filters between compressor and receiver. Without downstream treatment, water shows up in every air line within 48 hours. Don't let the customer "install the dryer later", it never happens later.
Step 05
Condensate handling
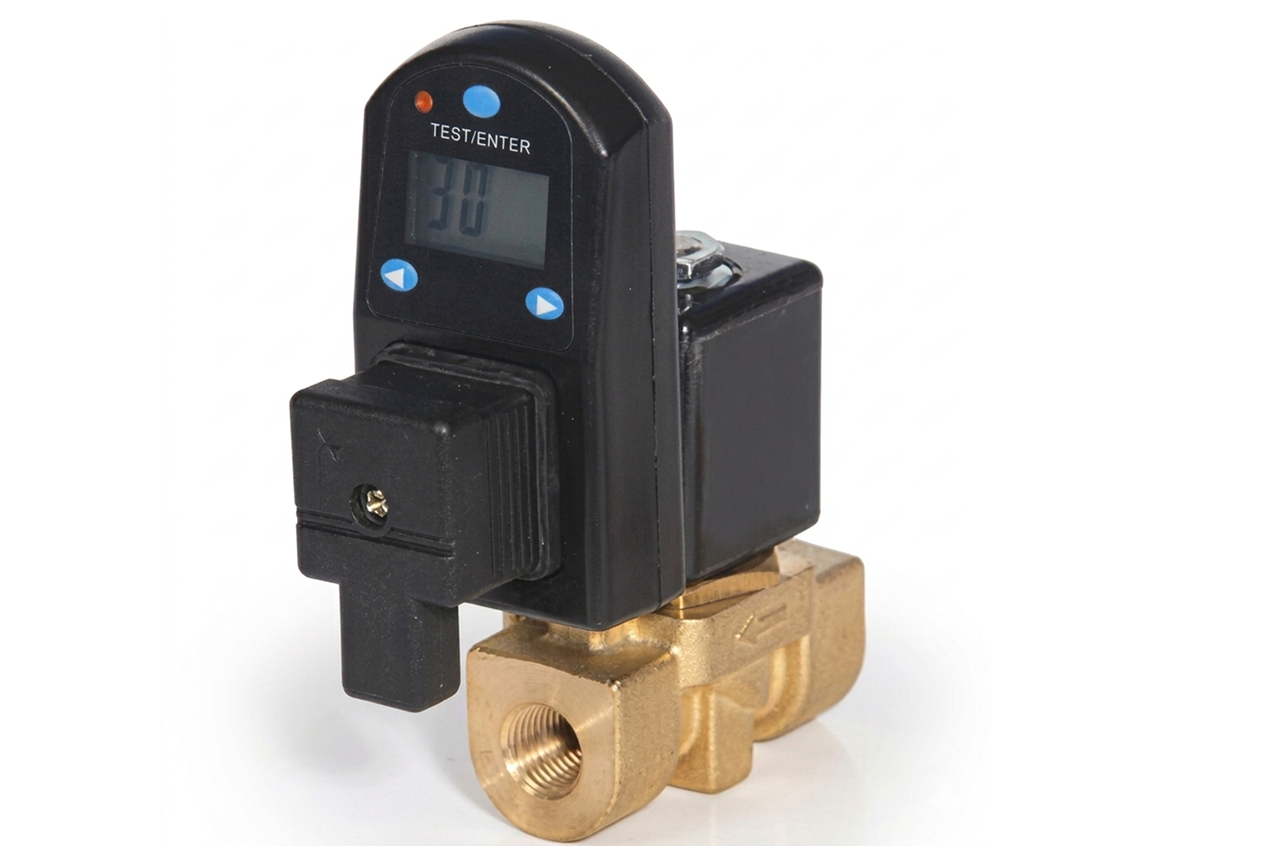
Compressor + dryer + receiver + filter all generate condensate. Quote an electronic-timer drain on each, route through an oil-water separator (OWS), route OWS effluent to a permitted discharge, most regions require permitted disposal for oily condensate, not the sanitary sewer.
Step 06
Document the service schedule on day one
Hand the customer the manufacturer's oil-change, filter-change, and rebuild intervals + SPC part numbers at install. The MRO revenue starts here; if the customer doesn't have the parts list from SPC, the next service goes to whoever does.
Troubleshoot · top failures

Most returns trace to one of these causes.

Symptom
Most likely cause
Fix
Compressor shutting down on high discharge temperature.
Compressor-room ambient over 100°F (most common), inadequate cooling-air flow recirculating heat, or oil cooler fouled with dust on air-cooled units.
Check ambient first, if the room is hot, fix the room before troubleshooting the compressor. If ambient is OK, clean the oil cooler fins (huge difference, often missed). If still tripping, oil is degraded or the thermostatic oil-cooler valve is failing.
Oil consumption higher than expected.
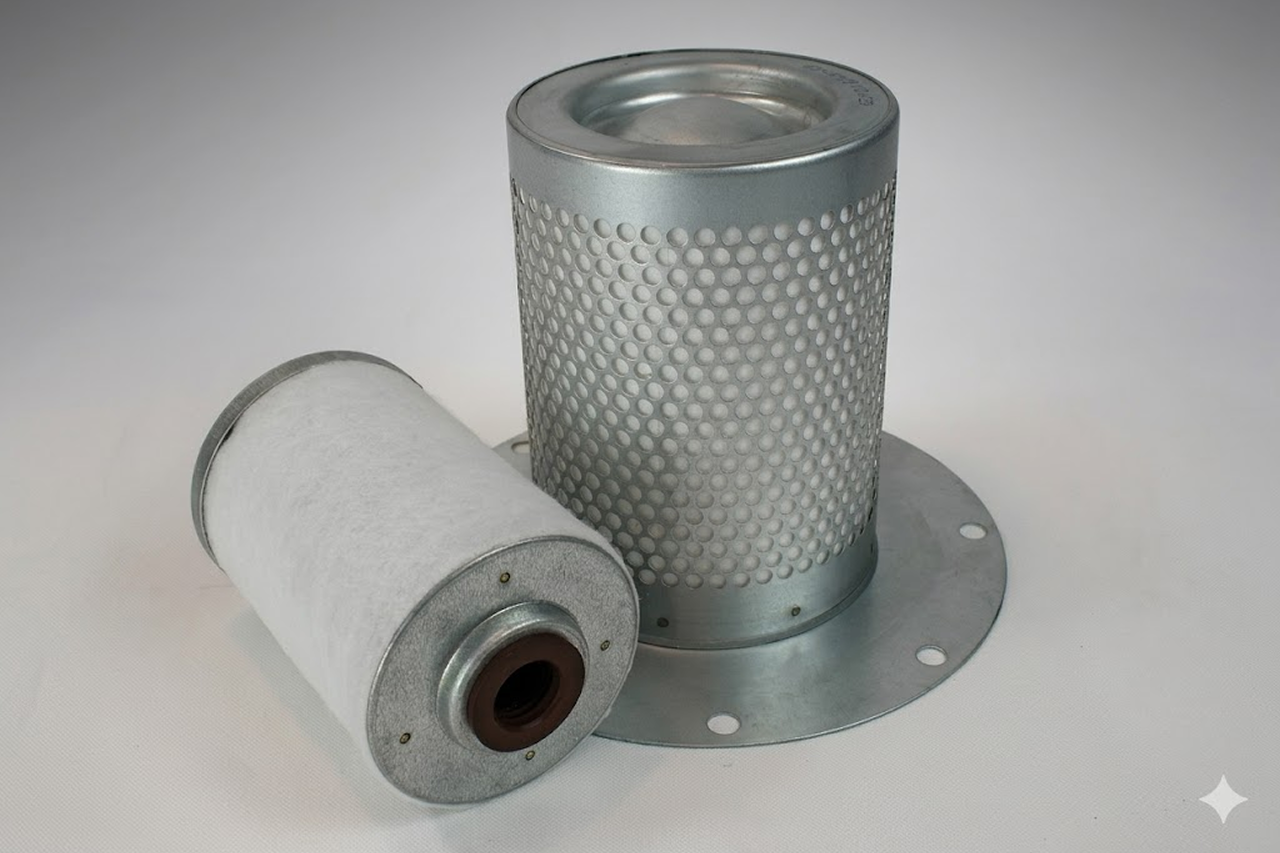
Air-oil separator element at end-of-life (typical at 4000-8000 hours, lets oil carry over into the air stream), separator drain line plugged (oil collects in separator instead of returning to sump), or oil-stop valve isn't seating during unload.
Pull and inspect separator element; replace if discolored or saturated. Verify drain return line flowing during operation. If both good, the oil-stop valve needs service.
Pressure not building / cycling without reaching setpoint.
Major air-system leak downstream (most common,
ed-speed compressors are good at meeting demand, so failure to reach setpoint usually means leaks), undersized for actual demand, or intake filter clogged. Fix: Leak-survey the system first, typical plant runs 20-30% leak rate. If leaks are addressed and pressure still won't hold, the compressor is undersized. Check intake filter as last resort.
Loud knocking or unusual noise from the airend.
Bearing failure imminent. Rotary screw airends fail catastrophically when bearings let go, rotors contact, airend destroys itself, $15-40K rebuild.
Shut down immediately. Pull oil sample for analysis (wear metals confirm bearing material). Do NOT restart until the airend is inspected. This is the failure mode that justifies oil-analysis programs as preventive, wear metals trend up for months before bearings fail audibly.
Demand spikes are not being met.
Receiver tank too small for the demand profile,
ed-speed compressors need ride-through storage for transient peaks. Fix: Verify receiver against 3-5 gal/CFM rule. Adding a wet receiver between compressor and dryer is often cheaper than upsizing the compressor.

Get the right rotary screw compressor — fixed-speed on quote in 24 hours.

Send us the application — a specialist routes you to the correct tier with a configured part. Lead-times and pricing returned within one business day.

Open quote engine ↑