DISTRIBUTOR-FIRST SUPPLY PARTNER · SINCE 1999 Live · Pneumatic Automation System
SPC Company
Pneumatic Automation / Actuation / Vacuum End-Effectors / Vacuum Ejector / Generator
Layer 04 · Actuation Performance · SMC
What it is

Vacuum Ejector / Generator

Compare tiers ↓

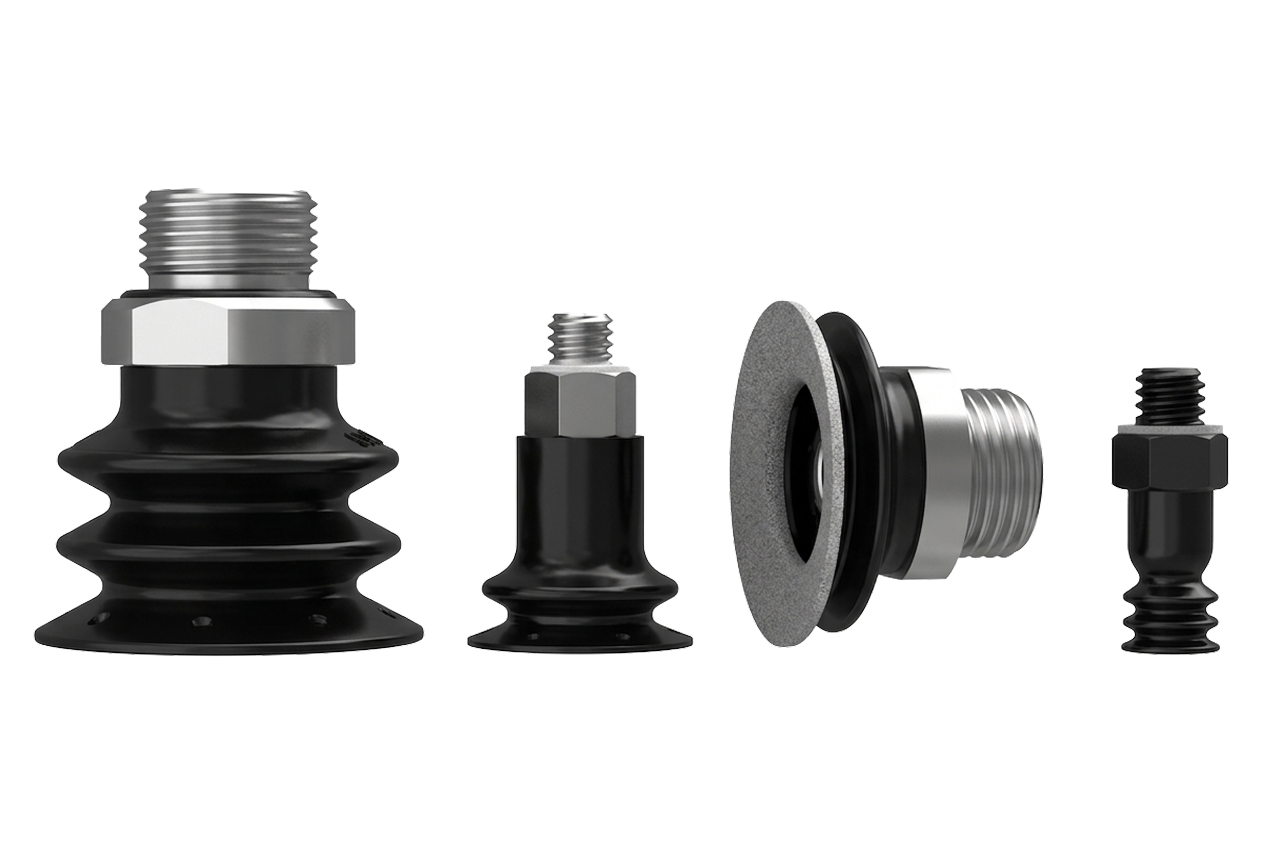
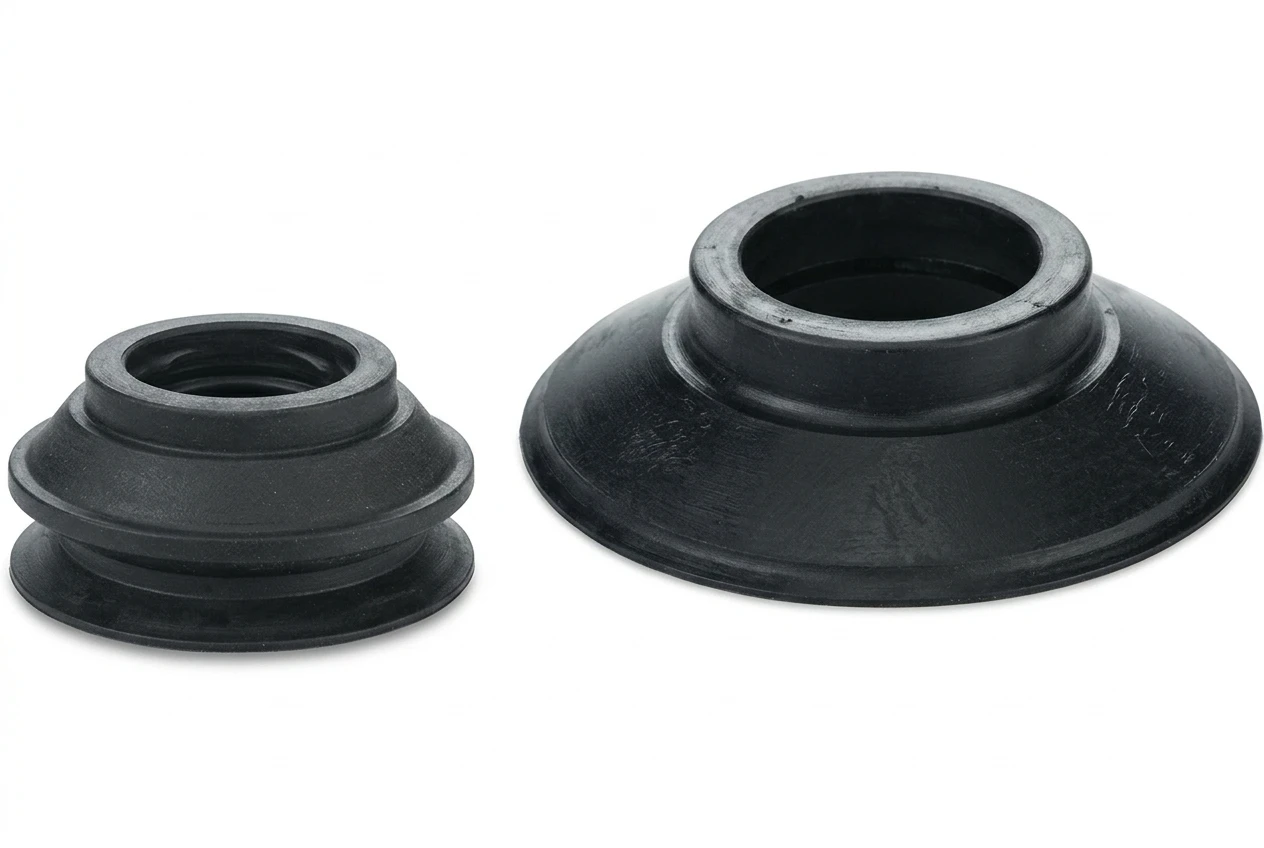
A vacuum ejector (also called a vacuum generator) is the air-powered vacuum source on a pick-and-place end-of-arm tool, it turns the machine's compressed air into suction at the gripper, with no separate vacuum pump motor, no electrical run, and no maintenance schedule beyond keeping the supply air clean. It is one quarter of the vacuum end-effector sub-system: ejector + suction cup + vacuum sensor + replacement cup, sold and quoted together as the working unit on every robotic arm, packaging gripper, sheet-metal beam, or pick-and-place head. Sized to the cup volume and cycle rate, the ejector mounts directly on the EOAT (end-of-arm tooling) plate, within inches of the cup it feeds.
Pictorial Representative vacuum ejector / generator
Vacuum Ejector / Generator — representative illustration
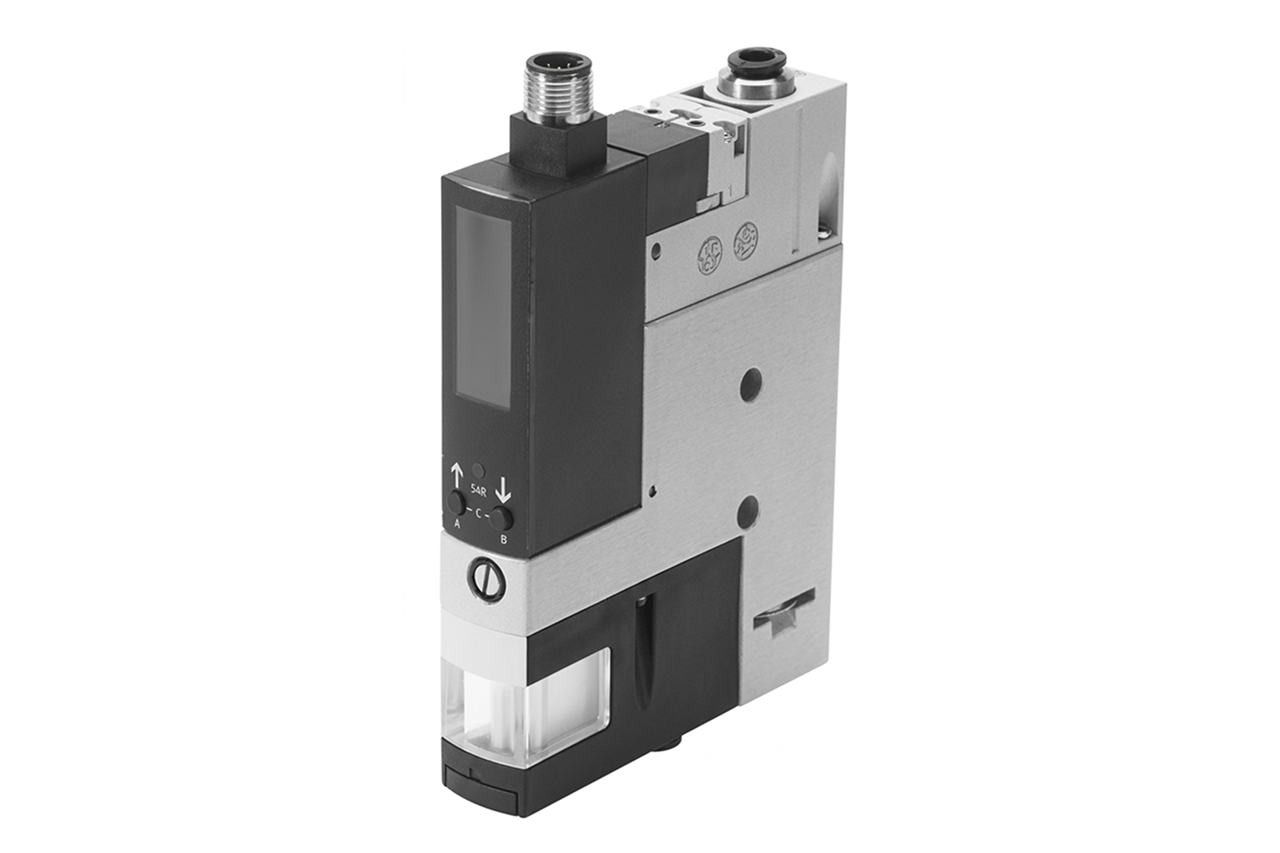
Real-world reference Representative vacuum ejector / generator
Vacuum Ejector / Generator — representative product photo
Why it's needed

Why this matters.

When an ejector is the right vacuum source, and when to spec something else. Review the points below.

01 · Key point
No motor, no maintenance.

A vacuum ejector turns compressed air into suction through a fixed nozzle, no motor, no vanes, no oil. Mounted within inches of the cup on the moving arm; the only wear part downstream is the cup itself.

02 · Key point
Vacuum on demand only.

Air flows only when the supply solenoid opens, typically 0.5–2 SCFM per ejector while generating, zero between cycles. The opposite duty cycle of a pump that runs continuously whether the gripper needs it or not.

03 · Key point
Hits –27 inHg in milliseconds.

Optimum supply is 58–72 PSI; achievable vacuum is –20 to –27 inHg (inHg = inches of mercury, the unit pneumatics uses for vacuum level). Reach time on a properly sized circuit is a few hundred milliseconds.

04 · Pro tip
Pick the stage to the surface.

Single-stage for smooth non-porous stock (sheet metal, glass, polished plastic). Multi-stage for porous or uneven (cardboard, bags, foam) where higher suction flow has to outrun continuous bleed-in. Energy-saving check-valve variant for long-dwell holds, cuts air 60–80%.

05 · Where not to use
Steady-state stationary vacuum.

CNC vacuum tables, multi-station fixturing, and other always-on holds run cheaper on a central pump. → Re-spec to vane pump for sustained flow: distributed ejectors win on moving grippers, lose on stationary loads.

06 · Where not to use
Supply pressure below 58 PSI.

Ejectors do not reach rated vacuum below their optimum window. Under-pressure shows up as missed picks, not as a gauge fault. → Re-spec FRL and drop size for a 65 PSI floor at the ejector inlet before adding more nozzle.

07 · Where not to use
Dirty or oily supply air.

Particulate or oil carryover fouls the nozzle within hours and kills vacuum. → 5-micron coalescing filter + precision regulator immediately upstream: non-negotiable on every ejector install.

Key selection criteria

What we need to spec it right.

From the machine spec sheet to the part number. Answer what you know, leave the rest blank, and send.

04Choose your priority  ·  core differentiator

Whatever your lever — performance, value, or price — SPC has the right brand.

Pick the priority; the quote desk handles the cross-reference.

01 Performance 1 brand
Install · 6 critical steps

The things that matter on the first install.

Step 01
Confirm supply pressure and air quality at the ejector inlet
Ejectors are rated 58-72 PSI optimum and 29-87 PSI working. Verify the FRL upstream is delivering clean dry air at the correct setting, particulate or oil in the supply will foul the nozzle and degrade vacuum within hours. Confirm tubing OD (outer diameter, the push-to-connect fitting size) matches the ejector inlet port and supports the rated SCFM without pressure drop.
Step 02
Mount the ejector as close to the suction cup as physically possible
Every cubic inch of hose between the ejector vacuum port and the cup is volume that has to be evacuated before grip is achieved. Mount within 6 inches of the cup on the EOAT plate. Long vacuum runs from a manifold-mounted ejector add measurable cycle delay.
Step 03
Plumb the vacuum side with minimum bends and matched tube ID
Use the largest tubing ID (inner diameter, the actual flow path) the cup fitting allows. Avoid sharp 90° fittings, multiple bends, and restrictive quick-couplers, every restriction reduces suction flow. On porous workpieces, plumbing restriction shows up directly as failed grip.
Step 04
Wire the supply solenoid valve to the PLC pick command
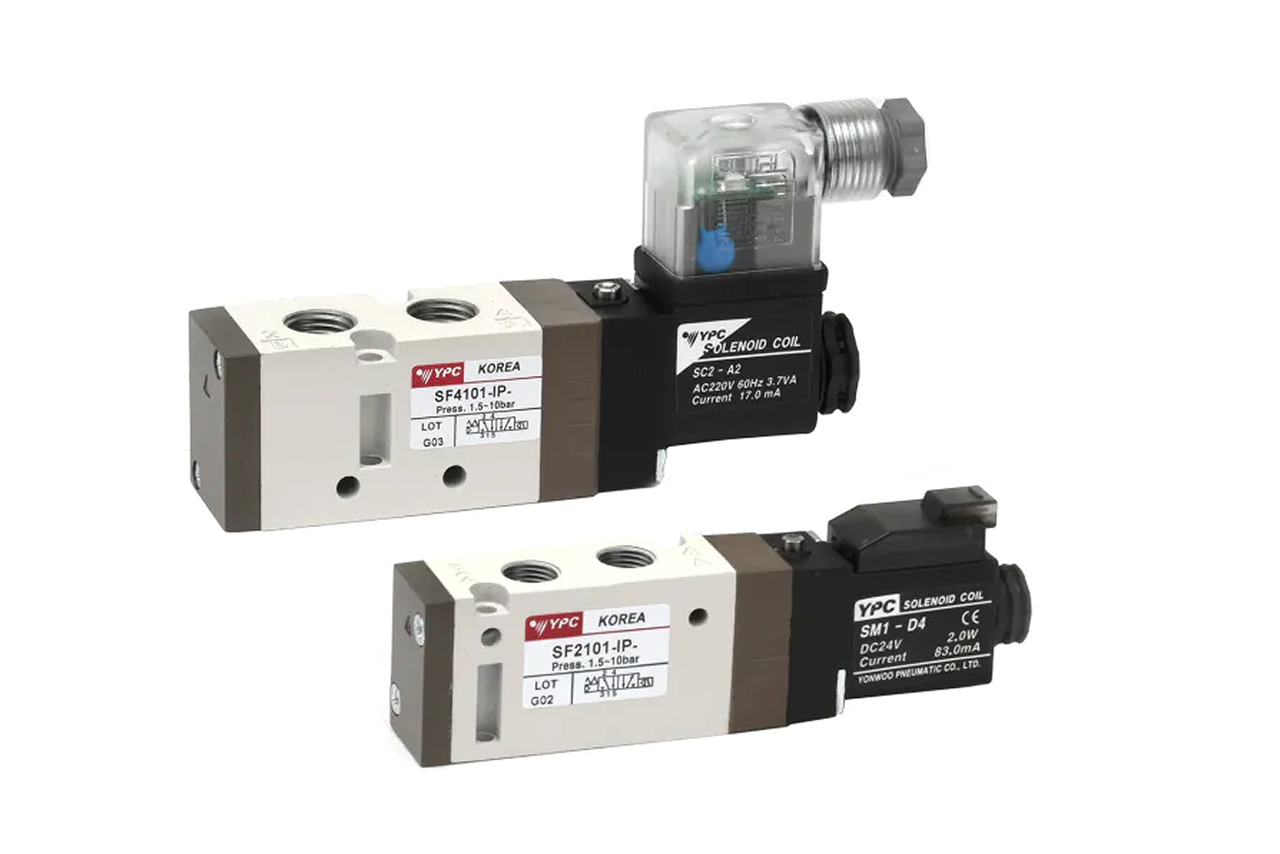
The ejector itself has no electrical input; air is gated by a solenoid valve upstream (integrated in the ejector block, or separate on the manifold). For integrated supply/release/blow-off blocks, wire both supply and release valves; the release pulse is what cleanly drops the part on cycle end.
Step 05
Install and aim the exhaust silencer
Multi-stage ejectors discharge through a silencer port. Confirm the silencer is unobstructed, not pointing at sensitive optics, and free of contamination at start-up. A blocked exhaust raises back-pressure inside the ejector and kills vacuum performance: check the silencer first on any degraded-suction call.
Step 06
Commission a dry-run cycle and verify vacuum reach time
Run the pick cycle without product. Measure with the paired vacuum switch or a temporary gauge tee'd into the vacuum line. If reach time exceeds budget, walk back: cup volume too large, ejector undersized, hose length too long, or supply pressure low. Validate with a loaded cycle on actual product before releasing the machine to production.
Troubleshoot · top failures

Most returns trace to one of these causes.

Symptom
Most likely cause
Fix
Ejector reaches partial vacuum but never hits the grip-confirm set point
Supply pressure below rated optimum, contaminated supply air fouling the nozzle, undersized ejector for cup volume × bleed-in rate, or a vacuum-side leak (cracked cup, loose fitting, damaged check valve).
Read supply pressure at the ejector inlet under cycle load, if it sags below 58 PSI, the FRL or supply line is undersized. Inspect supply filter for oil/water carryover. Soap-bubble test every vacuum-side fitting and the cup seal. If supply is correct and no leaks, upgrade to multi-stage or larger nozzle bore.
Vacuum reach time too long (robot missing picks at high speed)
Cup volume too large for ejector suction flow, restrictive plumbing between ejector and cup, fouled exhaust silencer raising back-pressure, or single-stage on porous workpiece.
Shorten the vacuum run, mount the ejector closer to the cup, maximize tubing ID. Replace exhaust silencer if discolored. If geometry is optimized, upsize to multi-stage or larger bore.
Air consumption higher than expected
Non-energy-saving ejector on long-dwell hold, supply pressure set above optimum (wasted air past 72 PSI), worn nozzle (years of contaminated air), or a vacuum-side leak forcing the ejector to run continuously.
If energized more than a few seconds at a time, upgrade to check-valve-held energy-saving variant. Lower supply to 65 PSI if currently 80+. Inspect for vacuum-side leaks, the silent air-waster.
Cup releases slowly at end of cycle (residual vacuum)
No blow-off circuit installed, check valve in energy-saving variant not releasing, or vacuum-side volume too large to vent quickly.
For lines >20 picks/min, specify an ejector with integrated blow-off, a brief positive pulse breaks the seal in milliseconds. If blow-off is already specified, verify the release valve is actually opening (wiring, signal, valve internal).
Vacuum present at ejector but the part still gets dropped
Vacuum reached at the ejector port but not at the cup (vacuum-side leak between ejector and cup), cup not seating fully (contamination, misalignment, wrong cup geometry), or grip force margin too thin in practice.
Tee a gauge into the vacuum line at the cup itself (not at the ejector) to confirm vacuum is reaching the seal. Inspect cup contact face and geometry vs. workpiece. Recalculate required cup count and size from part weight + acceleration, many "dropped part" investigations end at undersized cups, not the ejector.

Get the right vacuum ejector / generator on quote in 24 hours.

Send us the application — a specialist routes you to the correct tier with a configured part. Lead-times and pricing returned within one business day.

Open quote engine ↑